Линия производства упаковки EPS — высокоплотные защитные вкладыши
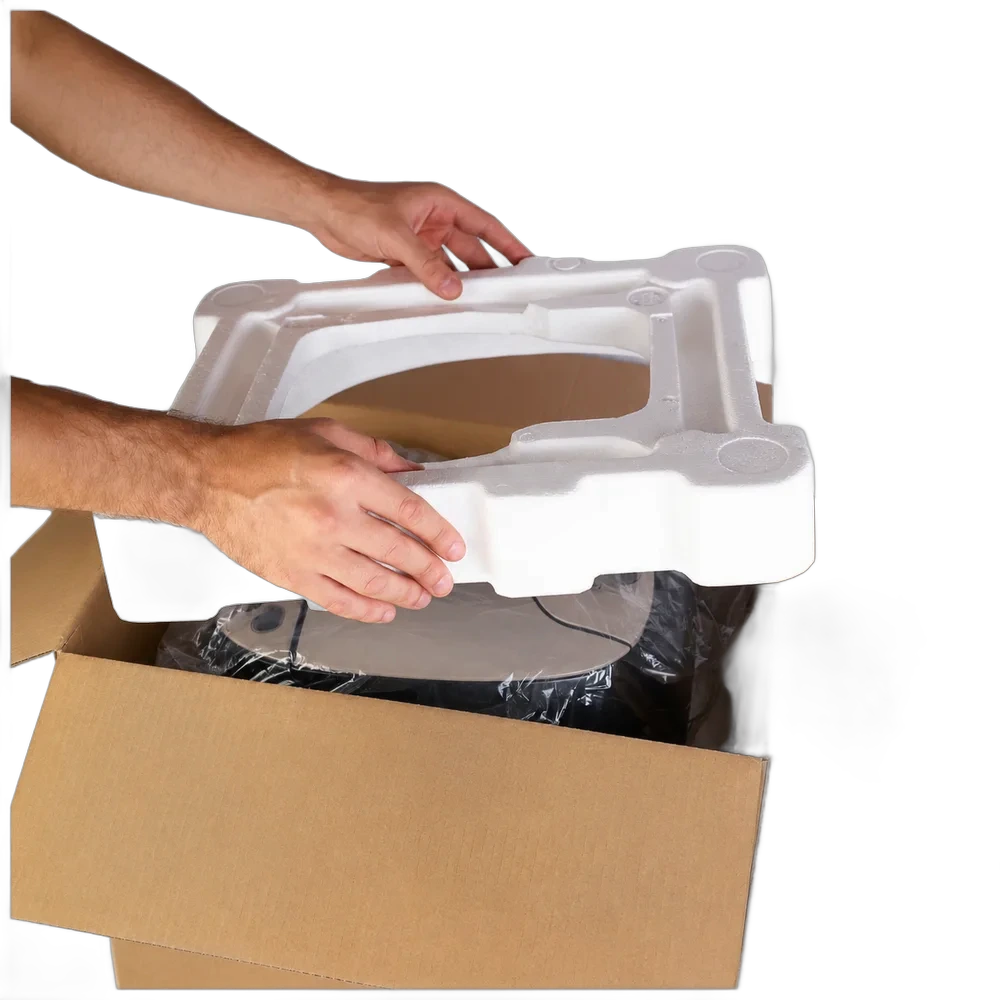
Линия производства упаковки EPS на базе высокоплотных (30-50 кг/м³) машин фасонного формования и пресс-форм вкладышей под заказчика для упаковки электроники, бытовой техники, автокомпонентов и медицинского оборудования. Разработана для прочности на сжатие >100 кПа и подтверждена испытаниями на падение по ISTA 3A / ASTM D5276, производительность 3 000-15 000 вкладышей в день. Спроектирована и изготовлена на собственных заводах, ввод в эксплуатацию на объекте заказчика.
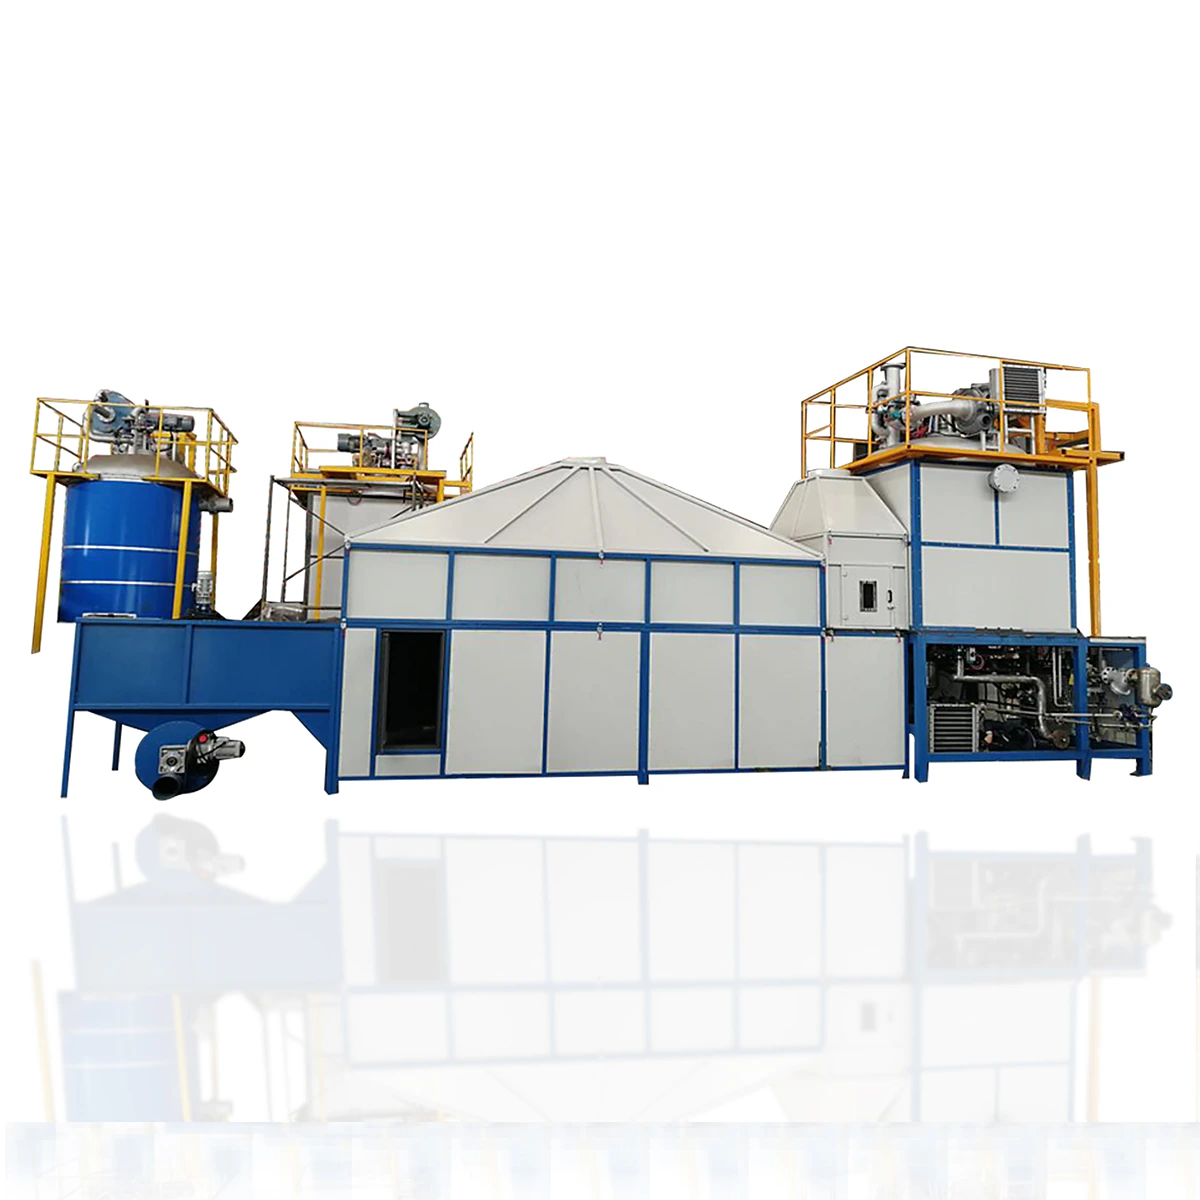
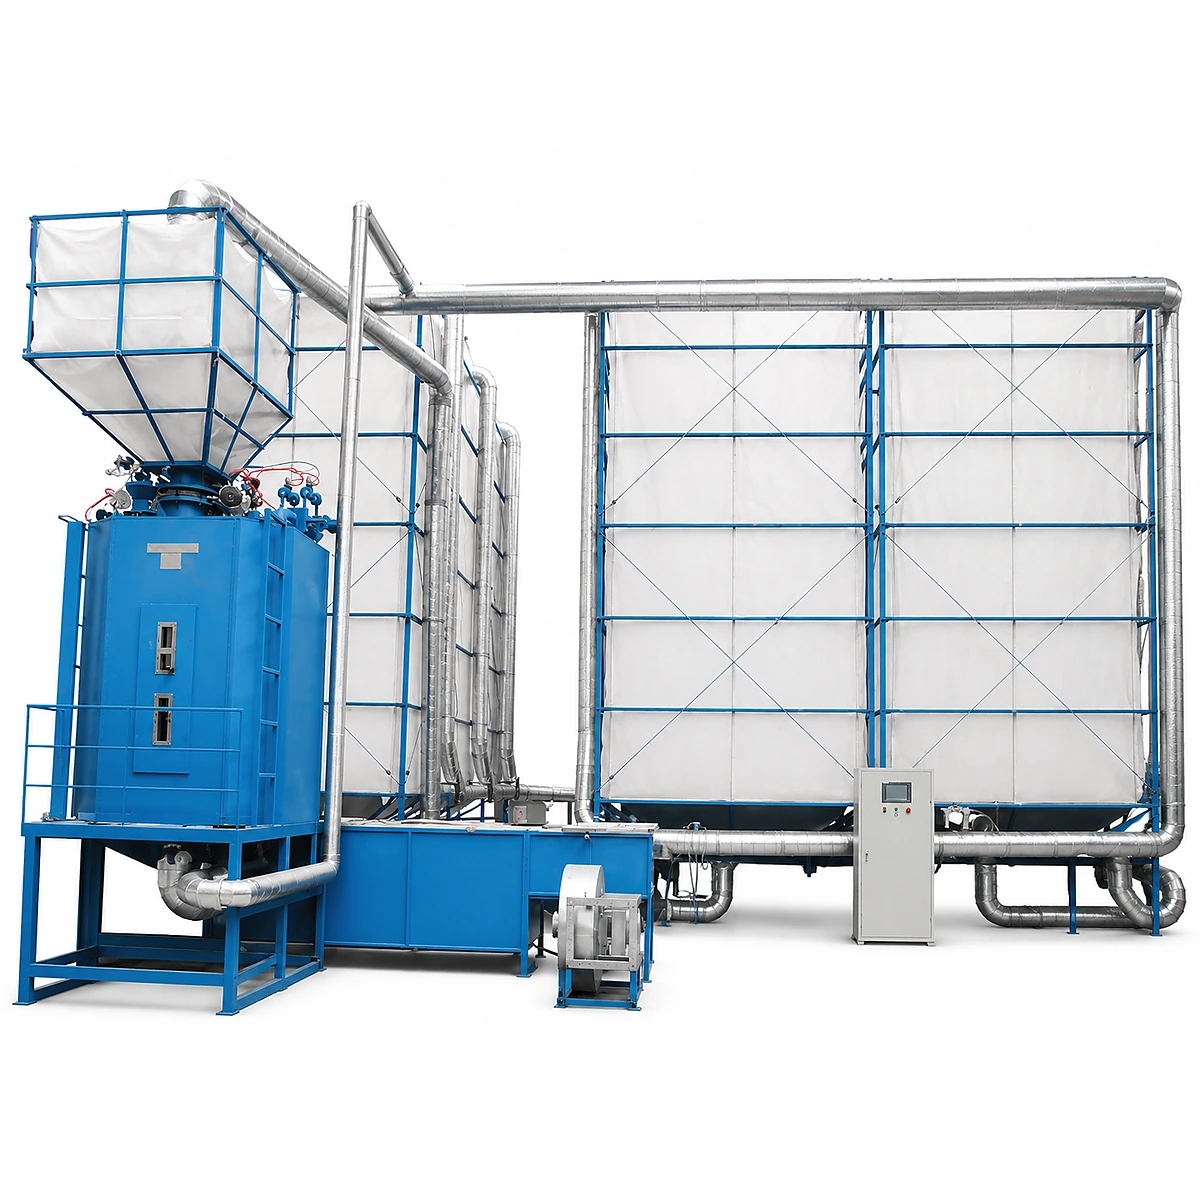
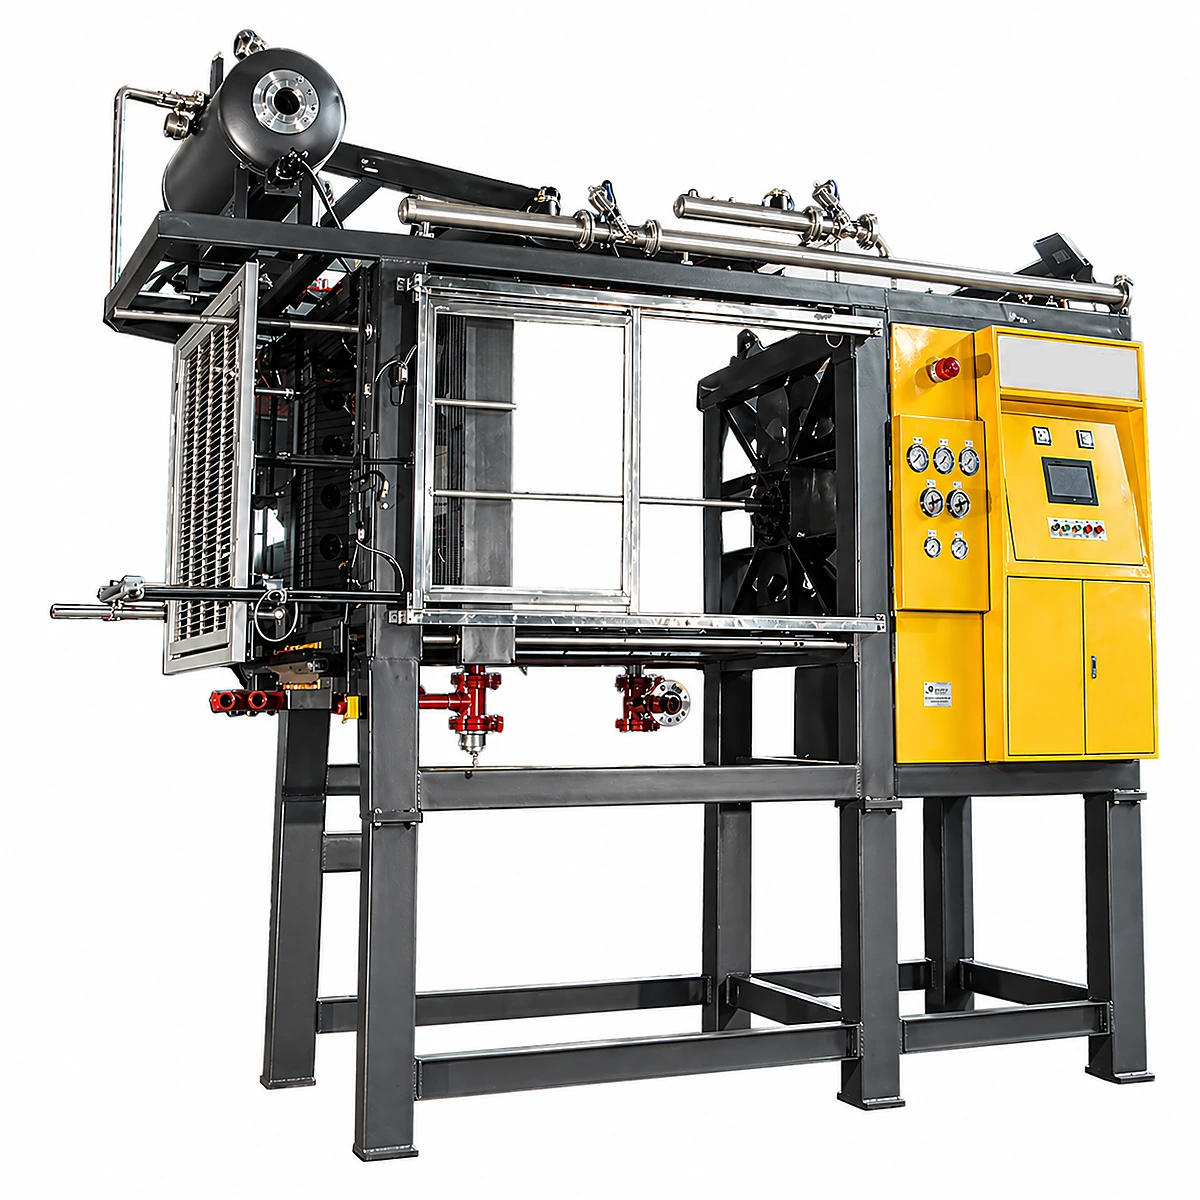
Линия производства упаковки EPS — это готовая установка, которая вспенивает сырые гранулы EPS и формует их паром в защитные упаковочные детали: высокоплотный предвспениватель, 6-8 силосов созревания, усиленные машины фасонного формования, пресс-формы вкладышей под заказчика и комплект коммуникаций (пар, охлаждающая вода, сжатый воздух, вакуум). Амортизирующие вкладыши формуются при плотности 30-50 кг/м³ — около 100 кПа сжатия при 30 кг/м³ и 200 кПа при 50 кг/м³ — за цикл 60-100 секунд, и одна линия выпускает от 3 000 до 15 000 вкладышей в день в зависимости от количества установленных формовочных машин. Формовочная машина в центре этой линии — упаковочная формовочная машина EPS — представляет собой усиленную машину фасонного формования: тот же цикл заполнения / пара / охлаждения / выброса, что и у стандартной машины EPS, но рассчитанную на паровую камеру 0,7-0,9 МПа вместо 0,4-0,6 МПа, поскольку вкладышам плотностью 30-50 кг/м³ со стенками 10-50 мм требуется больше энергии для спекания, чем рыбному ящику плотностью 16-22 кг/м³.
This Solution Solves
The real pain points operators in this industry face every day.
One failed drop test rejects the whole container
Electronics and appliance buyers test a sample against ISTA 3A or ASTM D5276 on arrival. A single fail sends the full shipment back, and the cost lands on the packaging supplier, not on the brand.
Density drifts between shifts, so compression strength drifts with it
Compression strength tracks density: about 100 kPa at 30 kg/m³ and 200 kPa at 50 kg/m³. A pre-expander run on operator feel makes parts that pass on Monday and fail on Friday.
Every account wants a different recipe, and the operator has to remember it
A plant serving industrial accounts juggles a different density, cycle time and steam time per buyer. Recipes kept on paper are the single largest source of scrapped batches.
Thick-wall inserts keep moving after they leave the mold
Walls of 10-50 mm shrink for hours after demolding. Parts measured at the machine pass; the same parts fail the buyer incoming check two days later.
How We Solve It
Specific technical answers ChinaEps engineers into this production line.
1
Challenge
The batch has to prove ISTA 3A / ASTM D5276 compliance before it ships
Our Answer
An in-line compression tester verifies >100 kPa at 10% strain during production, and the 4-machine layout adds a 10-30 m² on-site drop-test lab so the sample test happens before the container is loaded.
Differentiator
A test record per shipment, not one certificate per year.
2
Challenge
Holding density inside the 30-50 kg/m³ window batch after batch
Our Answer
Pre-expander steam pressure is controlled to the recipe rather than to the operator, and every batch is lot-coded through 6-8 aging silos with 24-48h aging before it reaches a molder.
Differentiator
Traceability per silo, from bead lot to finished insert.
3
Challenge
Switching between buyer-specific recipes without re-teaching the line
Our Answer
The PLC recipe library stores 100+ buyer recipes (density / cycle / steam time / cooling). The operator selects the buyer ID and the machine runs the locked recipe.
Differentiator
Recipe changeover is a selection, not a setup.
4
Challenge
Dimensional stability on 10-50 mm thick walls
Our Answer
A reinforced steam chest holds 0.7-0.9 MPa against a standard 0.4-0.6 MPa to fuse thick walls on a 60-100 second cycle, then 5-10 minutes of extended cooling before stacking.
Differentiator
Dimensions checked after cooling, not at the mold.
What This Line Produces
End products this turnkey line is engineered to manufacture.
TV / monitor corner inserts
Laptop / tablet packaging
Refrigerator / washing machine corner blocks
Air-conditioner packaging
Automotive bumper / dashboard inserts
Medical equipment custom geometry
Industrial machinery packaging
OEM cushioning to customer drawings
Production Flow
From raw material to finished product — six stages, fully integrated.
Step 1
EPS Raw Material
High-grade beads from supplier, traceability lot-coded.
Step 2
Pre-expander
High-density 30-50 kg/m³ pre-expansion for cushioning strength.
Step 3
Aging Silo
24-48h aging with batch traceability per customer order.
Before equipment arrival, the buyer needs to prepare the following on-site infrastructure.
Floor area
600-1,000 m²
Ceiling height
>= 6 m
Electrical
Three-phase 380V / 50Hz, 200+ kW
Steam supply
Local boiler 1-1.5 T
Cooling water
30-40 m³/h tower
Compressed air
6-7 m³/min compressor
Drop-test space
10-30 m² lab
Why ChinaEps for This Solution
Engineering specifically tuned for this application — not a generic line.
High-Density 30-50 kg/m³ Engineering
Cushioning compression strength is determined by density. We tune pre-expander + cycle for 30-50 kg/m³ — far higher than fish box, matching ISTA 3A / ASTM D5276 drop-test specs.
Per-Customer Batch Traceability
PLC silo routing + batch lot codes give per-shipment QC records. Critical for electronics / medical buyers who require traceability for liability.
Drop-Test Lab Integration
On-site ISTA / ASTM lab (Option 3) verifies every batch on-site before shipping. Reduces buyer return rate, increases per-shipment margin.
Reinforced Steam Chest
High-density requires higher steam pressure + longer hold. Our SM-1200/1400 reinforced chest handles 0.7-0.9 MPa vs standard 0.4-0.6 MPa.
Utility Consumption Calc
Steam · Air · Cooling Water
Per-equipment + total demand for sizing your boiler, compressor, and cooling tower.
Steam Consumption (3-machine cushioning line)
Equipment
Per Unit
Qty
Total
EPS Pre-expander (high-density)
150-250 kg/h
1
150-250 kg/h
High-density Molders
120-180 kg/h
3
360-540 kg/h
Pipeline loss (≈10%)
-
-
50-80 kg/h
Total Steam Demand
-
-
560-870 kg/h
RecommendationRecommended boiler: 1-1.5 T/h (higher per-cycle than fish box due to density). Use 0.8T for 1-2 machines, 1.5-2T for 4+ machines.
Compressed Air Consumption
Equipment
Per Unit
Qty
Total
Pre-expander pneumatics
0.3-0.4 m³/min
1
0.3-0.4 m³/min
Molder clamping (heavy)
0.6-1.0 m³/min
3
1.8-3.0 m³/min
Auto conveying + stacker
0.5-1.0 m³/min
1
0.5-1.0 m³/min
Compression test pneumatics
0.2-0.4 m³/min
-
0.2-0.4 m³/min
Total Air Demand
-
-
2.8-4.8 m³/min
RecommendationRecommended air compressor: 6-7 m³/min at 0.8 MPa. Air storage tank 2-3 m³. Air dryer essential.
Cooling Water Consumption
Equipment
Per Unit
Qty
Total
High-density molders
4-6 m³/h
3
12-18 m³/h
Extended cooling conveyor
3-5 m³/h
1
3-5 m³/h
Pre-expander cooling
1-2 m³/h
1
1-2 m³/h
Total Circulating Water
-
-
16-25 m³/h
Actual Make-up Water (8h)
-
-
12-20 m³/day
RecommendationRecommended cooling tower: 30-40 m³/h. Cooling water pumps: 2 pcs. Water pool: 15-20 m³.
Container Plan
20GP / 40HQ Loading Configurations
Pre-engineered container loading for your line size — daily output 800-30,000+ pieces.
Local-purchase recommendation: Steam boiler, air compressor, cooling tower, and water tank are not shipped from China — local purchase saves freight, matches local voltage / certifications, and reduces total project cost by 15-25%.
Frequently Asked Questions
What is an EPS packaging production line?
It is the complete set of machines that turns raw EPS beads into finished protective packaging: pre-expander, aging silos, shape molder, the insert molds, and the steam / cooling / compressed-air / vacuum utilities behind them. The line is defined by the density it runs — 30-50 kg/m³ for industrial cushioning inserts — because density sets compression strength, and compression strength is what the buyer drop test measures.
What machines does an EPS packaging production line need?
Five subsystems are mandatory: a high-density pre-expander, 6-8 aging silos, a reinforced shape molder (SM-1200 / SM-1400), the buyer-specific insert molds, and the utility set (1-1.5 T steam boiler, 30-40 m³/h cooling tower, 6-7 m³/min air compressor, vacuum). The full turnkey configuration on this page lists 20 items, including compression tester, auto stacker, wrapper and waste crusher.
Which EPS packaging line do I need — industrial inserts, fish boxes, or fruit trays?
Pick by end product, because density and mold set differ. Industrial cushioning inserts for electronics, appliances, automotive and medical equipment run 30-50 kg/m³ on this line. Insulated seafood and ice boxes run far lighter on the EPS fish box production line. Ultra-light fruit trays and liners run multi-cavity molds with quick changeover on the fruit packaging line. The pre-expander, silos and utilities are shared engineering; the molder duty and molds are not.
Which molding machine makes EPS packaging?
A shape molding machine fitted with the buyer’s insert mold — SM-1200 (1,200 × 1,000 mm platen) or SM-1400 for larger inserts. For protective packaging it is specified differently from a standard EPS molder in three places: a reinforced steam chest holding 0.7-0.9 MPa against a standard 0.4-0.6 MPa, heavy-duty clamping for 10-50 mm wall sections, and a 60-100 second cycle instead of the 45-90 seconds a light box runs. Below roughly 30 kg/m³ a standard molder is adequate; at 30-50 kg/m³, which is where drop-test compression strength lives, it is not.
Do you manufacture the EPS packaging machines yourselves?
Yes. Eps Industry Engineering builds the pre-expander, the shape molders and the mold sets in its own plants — 10,000 m² across three sites in Jiangyin, Wenzhou and Dongguan — and integrates them with the silo, utility and handling equipment that completes the line. The management system is ISO 9001 certified and machines in the pre-expander and block cutting ranges carry CE certification issued by SGS. Ask for the certificate scope covering the specific model you are quoting, not a company-level statement.
Can your line meet ISTA / ASTM drop-test compliance?
Yes. Lot traceability + density consistency + on-site drop-test lab (Option 3) verify every batch meets ISTA 3A or ASTM D5276. We provide test certificates per shipment.
How is per-customer recipe managed?
PLC recipe library stores up to 100+ customer recipes (density / cycle / steam-time / cooling). Operator selects buyer ID, machine runs the locked recipe. No human error.
What is the cycle time for thick-wall inserts?
60-100 seconds. Thicker wall (>20mm) requires longer steam fusion. Optimization vs throughput is recipe-specific per buyer.
Do I need a separate boiler vs my existing fish box line?
If you already have 1T boiler, you can run small cushioning line on it. For 4-machine cushioning plant, 1.5T boiler is recommended.
How long does the line take to commission?
Equipment delivery 30-45 days + on-site installation 14-21 days. First product shipment typically 60-90 days after PO.
Tell Us Your Production Goals
Share your capacity targets, product specs, and budget — our engineers design the optimal line for your factory.