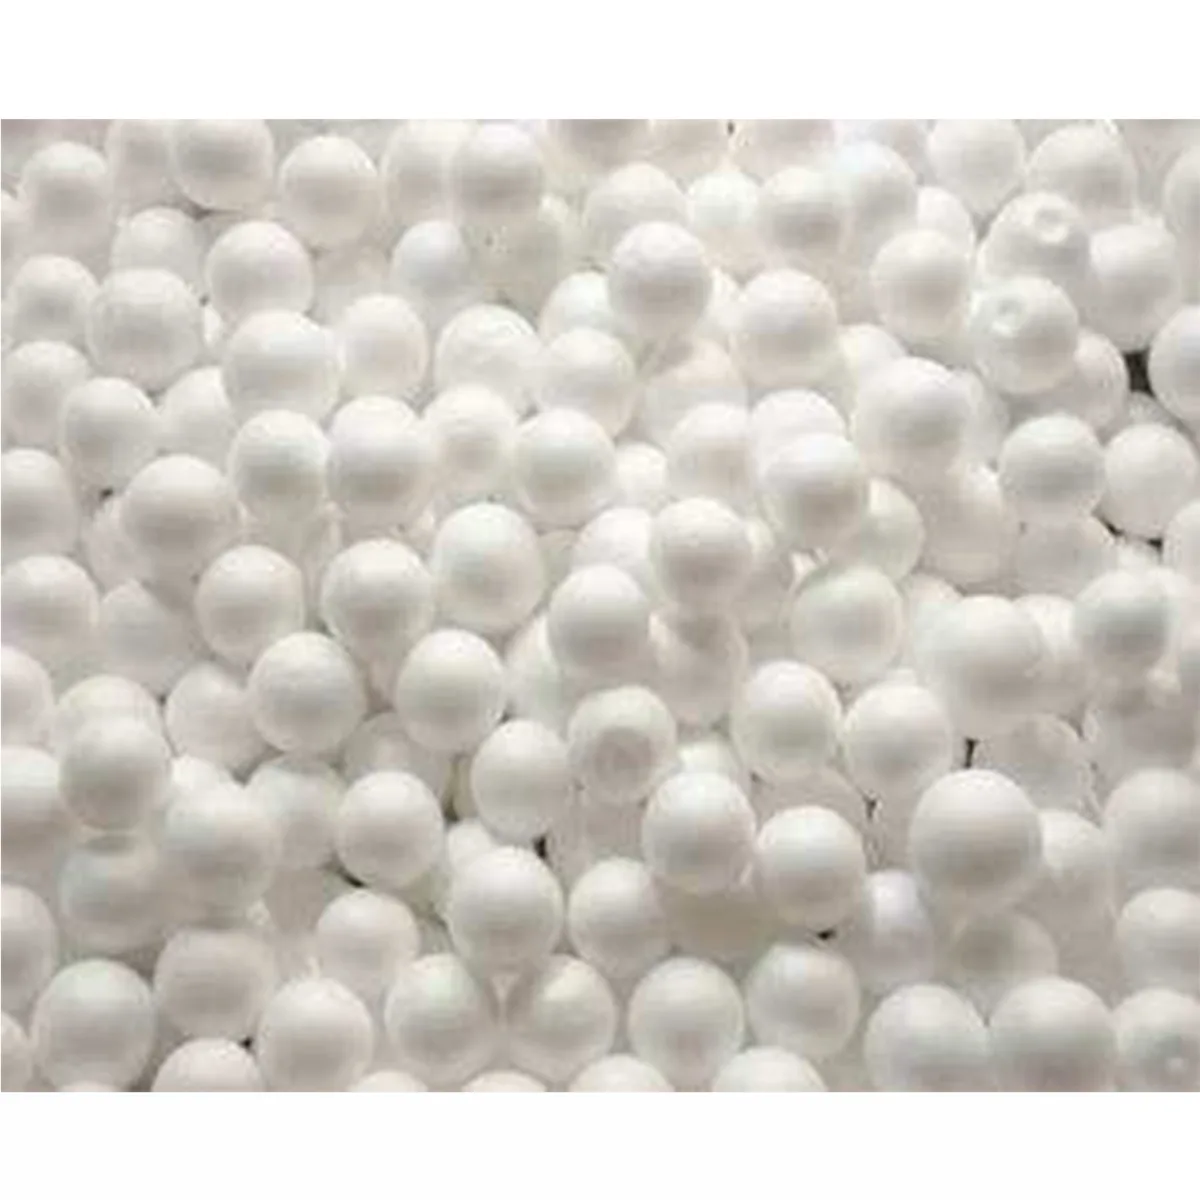
ETPU material is expanded thermoplastic polyurethane: solid TPU is foamed into elastic, predominantly closed-cell beads, then fused into lightweight molded parts. ETPU foam is best known for resilient footwear midsoles, but the same repeated-compression recovery is useful in sports protection, vibration damping, seals and cushioning.
This guide starts with the ETPU answer, then compares it with EPS and EPP. Choose ETPU when rebound, flexibility and repeated-load durability justify a premium material and a grade-specific molding process. Choose EPS for economical insulation or protective packaging, and EPP for reusable impact protection and automotive parts. Exact performance depends on the bead grade, molded density, part geometry and test method, so a supplier technical data sheet should control the final specification.
What Is ETPU Foam?
ETPU (expanded thermoplastic polyurethane, also written E-TPU) is an elastic bead foam made from a TPU base polymer. A supplier expands TPU into foam beads; a converter then fuses those beads into a molded component by steam-chest, heat-press or another grade-approved process. It is not simply a sheet of solid TPU with a different name. The foam structure lowers weight while retaining the rubber-like elasticity, abrasion resistance and resilience associated with TPU.
- Relationship to TPU: TPU is the base thermoplastic elastomer; ETPU is its expanded bead-foam form.
- Typical supply form: expanded beads for molding, or pre-molded sheets and components, depending on the supplier grade.
- Main advantage: high rebound and recovery through repeated compression, with good abrasion and chemical resistance.
- Main limitation: higher material and conversion cost than EPS or EPP, plus tighter grade, mold and process requirements.
ETPU Material at a Glance
| Question | Verified answer |
|---|---|
| Full name | Expanded thermoplastic polyurethane (ETPU or E-TPU) |
| Base material | Thermoplastic polyurethane (TPU) |
| Structure and form | Predominantly closed-cell, elastic beads fused into molded parts |
| Representative molded density | Approximately 80–240 kg/m³ across current BASF Infinergy footwear grades; individual grades and processes have narrower windows |
| Verified rebound examples | More than 55% by ISO 8307 ball rebound for the cited Infinergy comparison; current grade tables report pendulum rebound above 55% to above 75%, depending on grade and process |
| Key strengths | Elastic recovery, repeated-load resilience, abrasion resistance, tensile strength and chemical resistance |
| Typical uses | Footwear midsoles, sports and protective components, comfort parts, flooring, vibration damping and cushioning |
| Cost position | Premium versus commodity EPS and EPP; obtain a dated quote for the exact grade, bead form, order size, region and Incoterm |
| Main limits | Not a primary insulation foam; processing and long-term water, heat and chemical performance are grade-specific |
Data note: the density and rebound figures above are product-family examples, not universal ETPU constants. They come from BASF’s Infinergy product information accessed in October 2026. The previous page mixed three unsourced raw-material price ranges, so precise dollar-per-kilogram claims have been removed until a dated, region-specific supplier quotation is available.
1. Chemical Composition and Cell Structure
Understanding what each foam is made of — and how its cellular architecture forms — explains most of the performance differences you will encounter.
EPS — Expanded Polystyrene
EPS starts as solid polystyrene beads impregnated with a blowing agent (typically pentane). During pre-expansion, steam heats the beads to 80–110 °C, vaporizing the pentane and inflating the beads up to 50 times their original volume. The resulting cells are closed, roughly spherical, and filled with air once the pentane diffuses out over 24–48 hours of aging. EPS is a thermoset-like thermoplastic: while technically thermoplastic, the fused-bead structure does not re-melt into a uniform phase easily, making it effectively a single-use material in most recycling streams.
EPP — Expanded Polypropylene
EPP uses polypropylene copolymer beads expanded under high-pressure steam (typically 3–6 bar). The cell walls are thicker and more resilient than those of EPS because polypropylene is inherently tougher and more flexible than polystyrene. Crucially, EPP is a true thermoplastic: it can be re-melted, re-expanded, and recycled in closed-loop systems, which is increasingly important for automotive OEMs chasing sustainability targets.
ETPU — Expanded Thermoplastic Polyurethane
ETPU combines a TPU elastomer with a cellular bead structure. Commercial grades can be supplied as expanded beads and fused into parts by steam-chest molding, heat pressing or other supplier-approved methods. BASF describes its Infinergy ETPU as a predominantly closed-cell, elastic particle foam; the exact chemistry, bead density, hardness and molding window vary by grade.
When to choose ETPU material: shortlist it when a part must recover after repeated compression, provide elastic rebound, or retain flexibility over a wide operating window. Choose EPS instead when low-cost thermal insulation or one-way protective packaging is the priority. Choose EPP when multi-impact recovery, automotive use or returnable packaging matters but ETPU-level rebound is unnecessary. The performance, cost, application and processing sections below show the trade-offs.
ETPU Foam Properties: What the Numbers Mean
Density and Hardness
Density is not one fixed ETPU specification. BASF’s current Infinergy portfolio lists molded midsole densities from roughly 80 to 240 kg/m³, with different windows for steam-chest, autoclave, heat-press and supercritical-fluid injection processes. A lower-density grade can reduce part weight, while a denser or harder grade can support load and improve dimensional control. Compare parts only at stated density, hardness and test conditions.
Rebound and Energy Return
Rebound describes how much mechanical energy a specimen returns after impact; it is not a universal percentage that can be compared without a method. BASF reports more than 55% for a cited Infinergy specimen under ISO 8307 ball rebound and publishes grade-specific pendulum values above 55% to above 75%. Those results replace the old, unsupported claim that ETPU simply “returns 55% more energy.” For footwear or protective parts, request the supplier’s method, molded density, conditioning and specimen geometry.
Compression Set and Fatigue
Compression set measures the permanent thickness loss after a specimen is compressed for a defined time and temperature, then allowed to recover. Lower is better, but the result changes with grade and conditions. Current Infinergy grade tables, for example, state the compression, temperature and duration alongside the result. Repeated-impact or fatigue claims should likewise come from cyclic testing on the intended molded density rather than from a generic material label.
Hydrolysis, Temperature and Oil Resistance
Do not treat every TPU chemistry as equally resistant. Polyether-based TPU grades are generally selected where hydrolysis and microbial resistance are important, while chemical and oil compatibility still depends on the formulation, concentration, temperature and exposure time. ETPU can remain flexible in cold conditions — BASF lists performance down to -20 °C for one Infinergy family — but a maximum continuous-use temperature must come from the exact grade data sheet. For wet, hot or oil-exposed industrial parts, validate the candidate grade in the actual fluid and duty cycle.
2. Mechanical Properties Comparison
The following table summarizes the key mechanical properties at typical production densities. Note that all three foams can be produced across a range of densities; the values below represent the most common commercial grades.
| Property | EPS | EPP | ETPU |
|---|---|---|---|
| Typical Density Range (kg/m³) | 10 – 35 | 20 – 120 | 80 – 240 in current BASF footwear-grade examples |
| Compressive Strength at 10% (kPa) | 50 – 200 | 30 – 800 | Grade and test-method specific |
| Energy Absorption (single impact) | Good | Very Good | Excellent |
| Energy Absorption (repeated impact) | Poor — fractures | Excellent — recovers >90% | High recovery; verify by grade and cyclic test |
| Tensile Strength (kPa) | 150 – 400 | 300 – 1,200 | Grade and molded-density specific |
| Elongation at Break (%) | 2 – 5 | 10 – 40 | Grade-specific; one cited Infinergy 230 result is 280% |
| Thermal Conductivity (W/m·K) | 0.030 – 0.038 | 0.034 – 0.045 | Confirm with the selected grade supplier |
| Max Service Temperature (°C) | 80 | 130 | Grade-specific; do not infer from the TPU family name |
| Chemical Resistance | Poor (solvents) | Good | Good for suitable grades; test the actual chemical exposure |
What the Numbers Mean in Practice
EPS wins on thermal insulation and ultra-low density — making it the default choice for construction insulation boards, cold-chain packaging, and disposable protective packaging where single-impact protection is sufficient. Its brittleness, however, means it fractures upon repeated loading.
EPP excels in multi-impact scenarios. An EPP automotive bumper core can absorb a 5 mph parking-lot collision and recover its shape for the next one. Its broader density range also allows engineers to dial in specific stiffness targets, from soft seat cushions to rigid structural cores.
ETPU is selected when elastic rebound and recovery under repeated loading matter. BASF’s published comparison shows its Infinergy grade outperforming the cited EPP, EVA and EPE specimens in rebound testing, but that is a product-and-test comparison rather than proof that every ETPU grade outperforms every competing foam. Its rubber-like elasticity, abrasion resistance and grade-dependent chemical resistance make it a candidate for footwear, vibration damping, gaskets and wearable protection.
3. Thermal Properties and Insulation Performance
For construction and cold-chain applications, thermal conductivity is often the deciding factor. EPS, with a thermal conductivity as low as 0.030 W/m·K at 15 kg/m³ density, remains the most cost-effective insulation foam per R-value dollar. EPP is roughly 15–25% less thermally efficient than EPS at equivalent thicknesses, which generally rules it out for primary insulation in walls and roofs unless its mechanical advantages are also needed. ETPU is the least thermally efficient of the three and is rarely specified for insulation purposes.
However, EPP has an important thermal advantage: its higher service temperature (130 °C vs. 80 °C for EPS) makes it suitable for under-hood automotive insulation, HVAC ducting, and applications near heat sources where EPS would soften or deform.
4. Cost Comparison
Cost must be evaluated at three levels: raw material, processing and total part cost. Public list prices are not a reliable basis for comparing these bead foams: grade, density, order size, region, Incoterm and contract date can all change the result. The previous version of this page quoted three conflicting ETPU dollar ranges without a dated supplier source; those figures have been removed.
| Cost Factor | EPS | EPP | ETPU |
|---|---|---|---|
| Raw Bead Cost Position | Lowest of the three in typical commodity applications | Higher than EPS | Premium; request a dated, grade-specific supplier quote |
| Processing Equipment Investment | Low – Medium | Medium – High | High |
| Energy Cost per m³ of Finished Foam | Low | Medium (higher steam pressure) | Grade- and process-dependent |
| Mold Cost | Low (aluminum) | Medium (steel, tighter tolerances) | High (precision steel) |
| Quote Must State | Grade, bead density, volume, region and Incoterm | Grade, bead density, volume, region and Incoterm | Grade, bead form, molded target, volume, region and Incoterm |
The purchase price is only one input to lifecycle cost. For a fair comparison, test permanent deformation, rebound retention and failure after the expected number of load cycles, then add scrap rate, molding time, tooling, warranty exposure and end-of-life handling. ETPU can justify its premium when repeated recovery is a functional requirement; it is usually unnecessary when the part only needs low-cost insulation or one-time impact protection.
5. Application Matrix
The following matrix maps each material to its strongest application areas, rated from not recommended (–) through acceptable (•) to ideal (☆).
| Application | EPS | EPP | ETPU |
|---|---|---|---|
| Building Insulation Boards | ☆ | • | – |
| Cold-Chain / Food Packaging | ☆ | • | – |
| Consumer Electronics Packaging | ☆ | ☆ | – |
| Automotive Bumper Cores | – | ☆ | • |
| Automotive Seat Cores | – | ☆ | • |
| Sports Helmets | • | ☆ | ☆ |
| Athletic Footwear Midsoles | – | – | ☆ |
| Industrial Vibration Damping | – | • | ☆ |
| Reusable Transit Packaging | – | ☆ | • |
| Decorative Moldings / Cornices | ☆ | – | – |
| Geofoam / Civil Engineering | ☆ | – | – |
Common ETPU Foam Uses
Footwear Midsoles
ETPU is used where a midsole needs resilient cushioning and rebound over repeated steps. Select the grade by molded density, hardness, compression set and the brand’s own wear protocol. EVA remains a practical alternative when cost, smooth surface finish or established compression-molding capacity matters more than maximum rebound.
Protective Sports Equipment
Elastic recovery can suit pads and other reusable protective components. ETPU should not be substituted into a helmet or certified safety product on material reputation alone: impact attenuation, geometry, temperature conditioning and the finished assembly must pass the relevant product standard. EPP is a common alternative for multi-impact structures; EPS remains common where controlled crushing is required.
Industrial Vibration Damping
ETPU can isolate repeated vibration or cushion cyclic loads when the selected grade retains elasticity under the operating temperature and chemical exposure. Do not use it without validation near hot surfaces, aggressive fluids or sustained static loads. Rubber, solid TPU and EPP are alternatives depending on frequency, load, environment and cost.
Seals and Cushioning
ETPU can serve in cushioning blocks and selected gasket-like parts where recovery and abrasion resistance matter. It is not automatically a fluid-tight seal: bead fusion, surface skin, joint design and compression determine leakage. Solid TPU, elastomeric rubber or another closed-cell foam may be better when sealing pressure or water ingress is the primary requirement.
6. Processing Equipment Differences
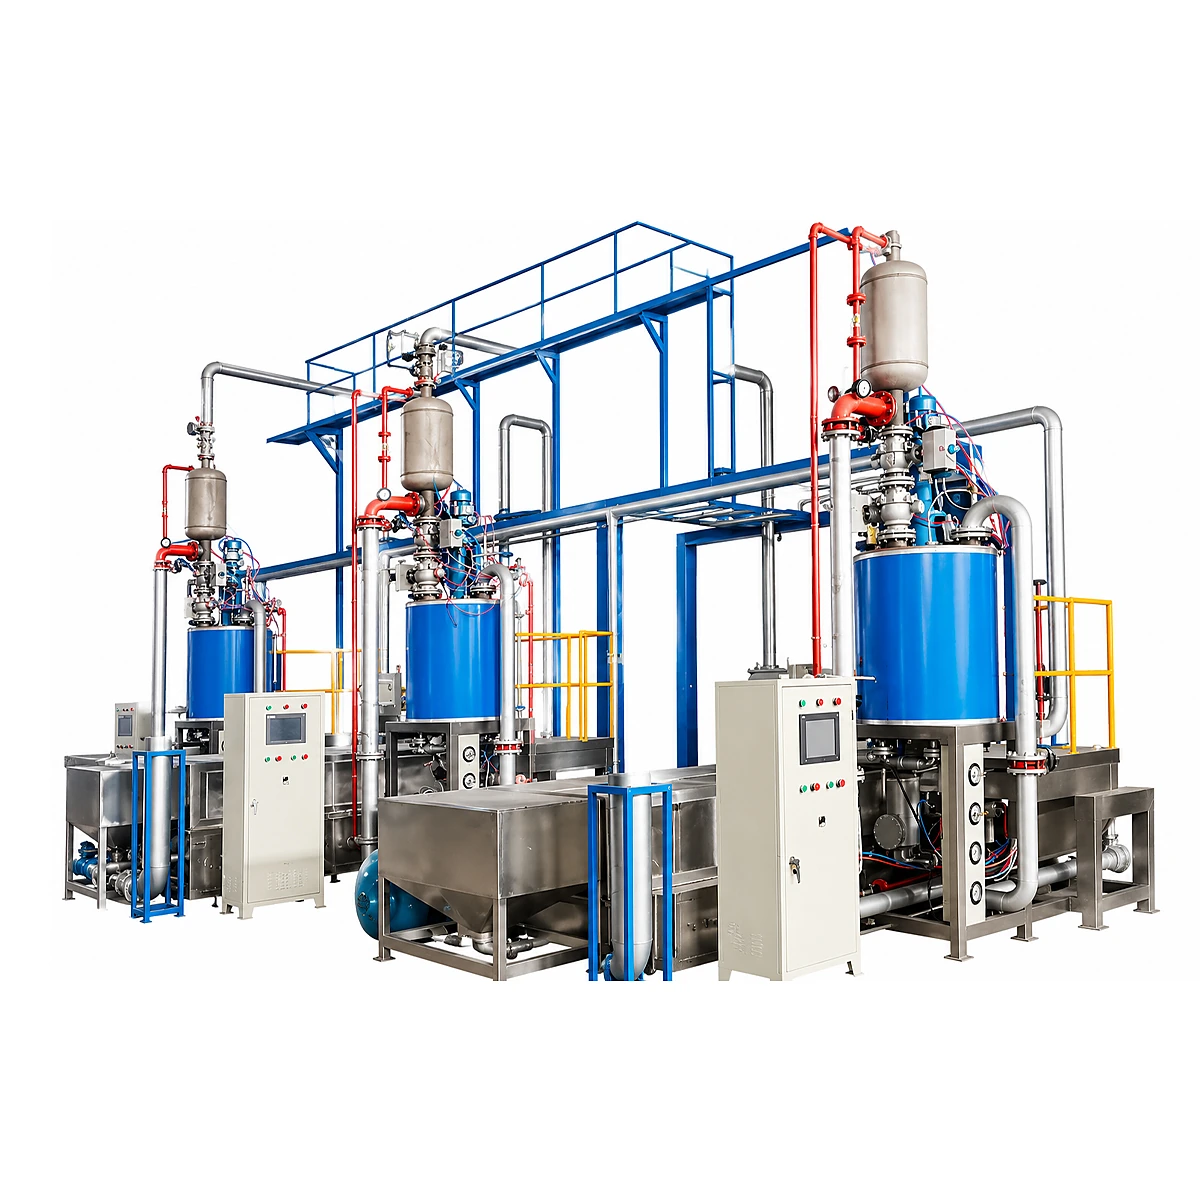
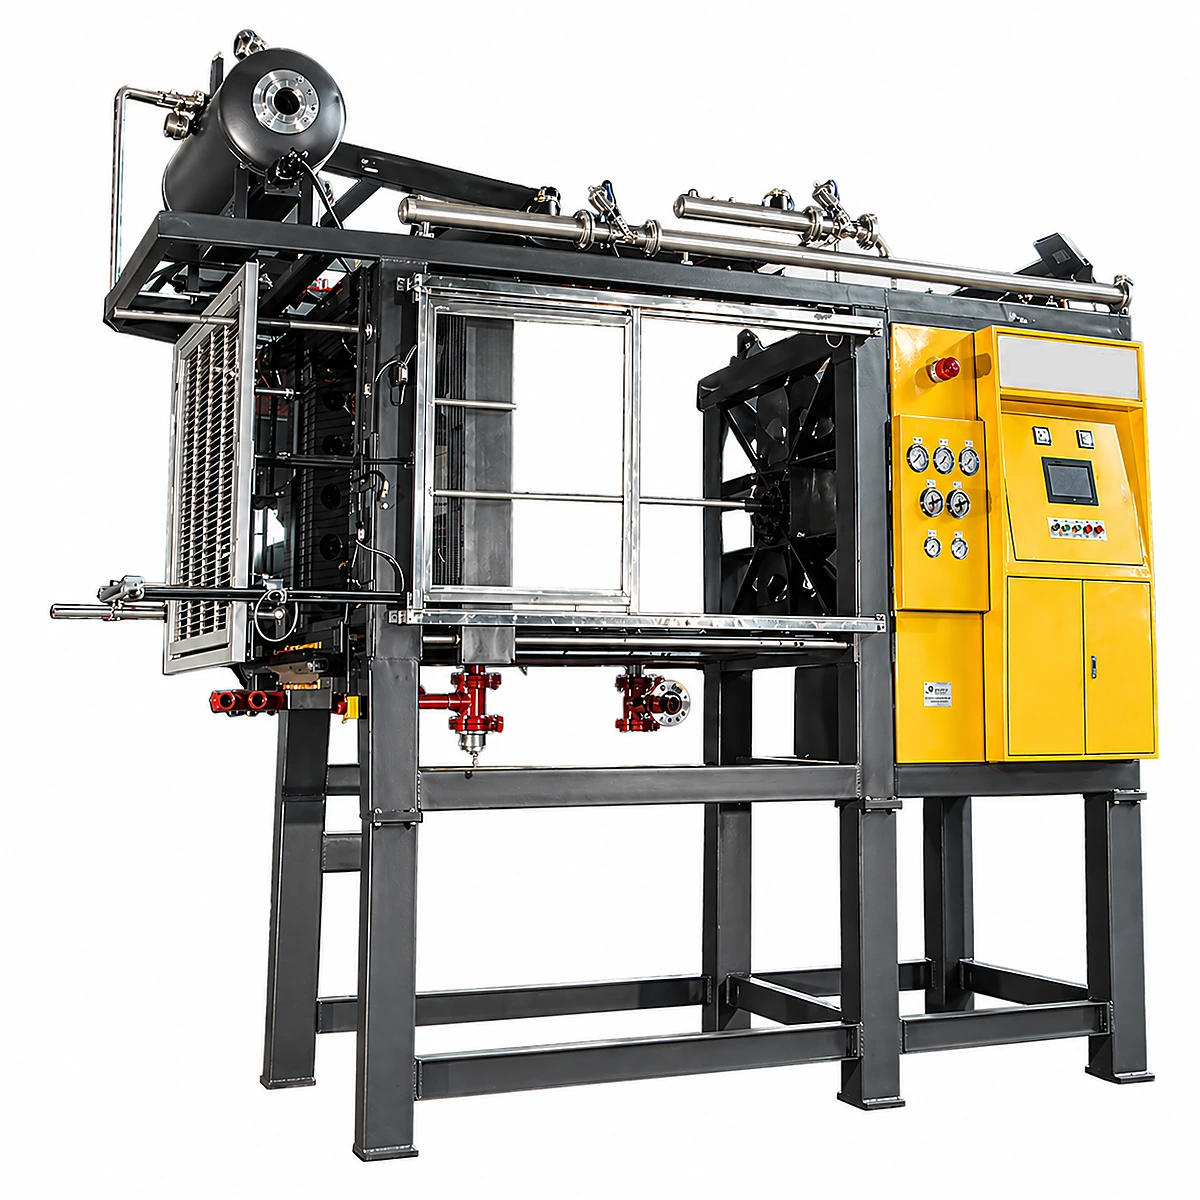
The machinery required to produce each material differs substantially — a critical consideration for factory owners evaluating production line investments. ChinaEps manufactures complete production lines for both EPS and EPP processing. You can explore the full range of equipment on our products page.
EPS Processing Line
- Pre-Expander: Batch or continuous pre-expander using low-pressure steam (0.5–1.0 bar) to expand raw beads to target density.
- Aging Silos: Expanded beads rest for 12–48 hours to allow pentane diffusion and internal pressure stabilization.
- Block Molding Machine: Beads are fed into a large rectangular mold, fused with steam, and cooled under vacuum to form large blocks (typically 1.0 × 1.2 × 4–6 m).
- Block Cutting Line: Hot-wire or CNC cutting systems slice blocks into boards, sheets, or custom shapes.
- Shape Molding Machine: For custom-shaped parts (packaging inserts, helmets, decorative elements), beads are molded directly into final-shape tooling.
EPP Processing Line
- High-Pressure Pre-Expander: EPP requires significantly higher steam pressure (3–6 bar) and often a counter-pressure process in the mold.
- Pressure Aging Tanks: Unlike EPS open-air silos, EPP beads are often aged under controlled air pressure to improve bead quality.
- Shape Molding Machine with Crack-Fill: EPP shape molding uses a specialized crack-filling technique where the mold opens slightly to accept beads, then closes for steam fusion. Machines require higher clamping force and more robust steam systems.
- Autoclave (for some grades): Certain high-density EPP grades require autoclave pre-expansion rather than continuous steam expansion.
ETPU Processing Line
- Bead manufacture or expansion: the material supplier produces an expanded TPU bead grade using its qualified foaming route. A converter buying ready-expanded beads does not necessarily perform this step.
- Part molding: supplier documentation lists steam-chest, heat-press, autoclave-sheet and other grade-specific routes. Steam pressure, filling method, cooling and water content affect fusion, appearance and molded density.
- Conditioning and quality control: cooling or post-treatment requirements must follow the selected grade and part design. Check density, dimensions, bead fusion, hardness, rebound and compression set against the approved process window.
Can Standard EPS or EPP Equipment Process ETPU?
Do not assume it can. A machine may look similar because bead foams can use steam-chest molding, but ETPU filling behavior, required chamber rating, mold design, heating and cooling sequence vary by supplier grade. BASF, for example, states that one Infinergy grade uses commercial steam-chest machines designed for at least 5 bar chamber pressure, while actual molding steam pressure depends on grade, geometry and density. That does not make every EPS or EPP machine ETPU-ready.
ChinaEps supplies and engineers EPS and EPP processing equipment. We do not present a standard ETPU production line in our current catalog. If your project is ETPU, first obtain the bead supplier’s processing sheet and required acceptance tests; then have the machine maker confirm chamber rating, filling system, mold, utilities and cycle in writing. For an EPS or EPP project, ChinaEps offers complete production line solutions from layout through commissioning.
7. Decision Framework: Choosing the Right Material
Use this step-by-step framework to narrow your material selection:
- Define the primary performance requirement. Is it thermal insulation, single-impact protection, multi-impact resilience, or elastic energy return? This alone often points to one material.
- Determine the operating temperature range. If the part will see temperatures above 80 °C, EPS is eliminated. Above 130 °C, all three bead foams are problematic and you may need alternative materials.
- Assess chemical exposure. Contact with solvents, fuels, or oils rules out EPS. ETPU handles the widest chemical spectrum.
- Calculate lifecycle cost, not just unit cost. Include replacement frequency, recyclability value, and warranty claims. EPP and ETPU often win on lifecycle cost despite higher unit cost.
- Evaluate production volumes. EPS tooling is the cheapest, making it ideal for low-to-medium volume custom shapes. EPP and ETPU tooling costs are higher but amortize well at automotive-scale volumes (50,000+ parts/year).
- Check regulatory and sustainability requirements. EPP is the most recyclable of the three. ETPU is gaining recyclability through chemical recycling pathways. EPS recycling infrastructure varies significantly by region.
Need help choosing between EPS and EPP equipment?
ChinaEps manufactures production lines for both EPS and EPP foam. Tell us your target application and volume — we’ll recommend the right material and machine configuration. Get a free material & equipment assessment →
8. Sustainability and Recyclability Outlook
Environmental regulations are reshaping material selection, particularly in the European Union and North American markets. Here is how each foam stands:
- EPS: Mechanically recyclable where collection infrastructure exists. Many jurisdictions are restricting single-use EPS food packaging but continue to permit EPS in construction (where it serves a long-term insulation function). Advances in chemical recycling (depolymerization back to styrene monomer) are improving the outlook.
- EPP: The strongest recycling story of the three. EPP can be ground, re-melted, and re-molded in a true closed loop. Major automotive manufacturers are implementing take-back programs. EPP is not subject to the same regulatory restrictions as EPS food packaging.
- ETPU: TPU is thermoplastic, and BASF identifies Infinergy as recyclable. Actual recovery still depends on whether the molded part can be collected, separated from adhesives and other materials, and accepted by a recycler. Treat material recyclability and local recycling access as separate questions.
9. Hybrid and Emerging Approaches
The market is also seeing hybrid solutions. Some automotive designs use an EPP structural core with ETPU comfort layers in seating applications. In packaging, EPP reusable crates with EPS insulation inserts combine the durability of EPP with the thermal performance of EPS. For manufacturers with the right equipment, offering multi-material solutions opens significant market differentiation.
If you are evaluating equipment that can handle multiple foam types, contact our engineering team to discuss flexible production line configurations.
Conclusion
There is no universally "best" foam — only the best foam for a specific application. EPS dominates on cost and thermal insulation. EPP wins on durability, multi-impact performance, and recyclability. ETPU leads on elasticity, energy return, and chemical resistance. Your selection should be driven by the application requirements, lifecycle economics, and the regulatory environment in your target market.
For guidance on the processing equipment needed for any of these materials, explore ChinaEps's full machinery catalog or review our turnkey production line solutions. If you would like a detailed comparison tailored to your specific product, our engineering team is available for consultation via the contact page.
Frequently Asked Questions
What is ETPU foam made of?
ETPU foam is made from thermoplastic polyurethane. The TPU is expanded into elastic foam beads, and those beads are fused into a molded part. Commercial formulations differ, so the exact TPU chemistry, bead density, hardness and additives must be confirmed on the grade data sheet.
Is ETPU the same as TPU foam?
Not exactly. TPU names the base thermoplastic polyurethane polymer. ETPU names an expanded, usually bead-based physical form of TPU. People sometimes use “TPU foam” as a broad category that can also include foamed sheets or injection-foamed parts, so a specification should state both the polymer and the required foam form.
What is ETPU material used for?
Common uses include athletic and casual footwear midsoles, sports and wearable protective components, comfort parts, industrial vibration damping, cushioning and selected gasket-like parts. It is chosen when elastic rebound, abrasion resistance or recovery through repeated compression matters more than minimum raw-material cost.
ETPU foam vs EVA: which is better for midsoles?
Neither is universally better. ETPU is attractive when rebound and repeated-load recovery are the priority. In BASF’s published ISO 8307 comparison, the cited Infinergy specimen exceeded 55% rebound while the cited EVA specimen measured 37%; the molded densities were not equal, so this is not a universal ETPU-versus-EVA rule. EVA can be preferable for lower cost, familiar processing, smooth molded surfaces or a specific hardness and feel. Compare candidate grades at the same part geometry and conditioning protocol.
Is ETPU foam waterproof?
ETPU beads can have a predominantly closed-cell structure, which helps resist rapid water entry into the cells, but a molded ETPU part is not automatically waterproof. Bead fusion, cut surfaces, seams, attachments and long-term immersion all affect ingress. Use a finished-part water-absorption or leak test for any outdoor, footwear or sealing application.
Can ETPU foam be recycled?
The TPU base is thermoplastic, and BASF describes Infinergy ETPU as recyclable. Practical recycling depends on collection, contamination, adhesives, mixed-material construction and access to a compatible processor. Ask the material supplier and local recycler to confirm the route before making a recyclability claim for a finished product.
Can the same machine produce both EPS and EPP?
In most cases, no. EPP requires significantly higher steam pressure (3–6 bar vs. 0.5–1.0 bar for EPS), different filling techniques (crack-fill molding), and more robust clamping systems. Some modern shape molding machines can be configured to handle both materials with modifications, but dedicated lines are recommended for optimal quality and throughput. Consult ChinaEps for dual-material line configurations.
Is ETPU worth the higher cost for packaging applications?
For single-use or limited-reuse packaging, ETPU is generally not cost-justified. Its advantages — elasticity, energy return, and chemical resistance — are most valuable in products with long service lives or demanding mechanical requirements. For reusable packaging that must survive hundreds of shipping cycles, ETPU may justify its premium over EPP, but a detailed lifecycle cost analysis is essential.
Which foam has the best fire resistance?
None of these foams is inherently fire-resistant. EPS is available with flame-retardant additives (EPS-FR) that achieve Class B or Class E fire ratings under EN 13501. EPP can also be formulated with flame retardants. ETPU has inherently better thermal stability than EPS but still requires flame-retardant formulations for fire-critical applications. Fire performance depends heavily on the specific formulation, density, and application context.
What is the minimum order quantity for starting an EPS or EPP production line?
ChinaEps supplies complete production lines ranging from small-scale starter configurations to high-capacity industrial lines. There is no minimum order quantity for raw materials to discuss — that is between you and your bead supplier. For machinery, a basic EPS block molding line can be configured for as little as $80,000–$150,000 depending on capacity requirements. Visit our product catalog for detailed specifications.
EPP foam density: what is the typical range?
EPP foam density typically ranges from 20 to 120 kg/m³, one of the widest usable density windows of any moulded bead foam. Low-density EPP around 20–45 kg/m³ is used for lightweight packaging and returnable dunnage, mid-density EPP of 45–80 kg/m³ suits automotive bumper cores and seat components, and high-density EPP above 80 kg/m³ is specified for structural and load-bearing parts. Because density is set during pre-expansion, EPP density is directly tunable by controlling steam pressure and residence time — a flexibility EPS cannot match. See our EPP foam density guide for the full density-by-application table, and our EPP manufacturing process guide for how EPP density targets are dialled in on the production line.
How does foam density affect the choice between EPS, EPP, and ETPU?
Density is a critical factor. If your application requires very low density (below 20 kg/m³), EPS is typically the only practical choice, as EPP and ETPU are difficult to expand to such low densities while maintaining structural integrity. For medium densities (20–60 kg/m³), both EPS and EPP are viable, and the decision shifts to mechanical requirements. For high-density applications (above 60 kg/m³), EPP and ETPU offer significantly better performance than EPS.
Are there environmental regulations that might restrict any of these materials in the near future?
Single-use EPS food packaging faces restrictions in parts of Europe, several US states, and some Asian markets. However, EPS for construction and industrial applications is not under the same regulatory pressure. EPP faces the fewest regulatory risks due to its excellent recyclability. ETPU is too new and too niche to be a regulatory target currently. Manufacturers should monitor local regulations in their target export markets and consider material flexibility in their production planning.
Sources & Further Reading
- BASF Infinergy ETPU portfolio: grade density, rebound and compression-set data
- BASF Infinergy Revolution: density, temperature range and processing routes
- BASF Infinergy 230 product information: test methods and molded-part properties
- Lubrizol TPU chemical and hydrolysis resistance guidance
- ASTM C578 Standard for Rigid Cellular Polystyrene
- EUMEPS European EPS Industry Association
- EPRO Plastics Recycling Europe
Related Reading
- The EPP Manufacturing Process: 6 Stages and the 8 Main Tools in EPP Production — Extended reading in the same cluster.
- EPP vs EPS Foam: How to Choose the Right Material — Extended reading in the same cluster.
- EPE vs EPS Foam: Differences, Sheets and Cost — Adds the fourth foam, soft expanded polyethylene, with water, temperature, solvent and fire comparisons.
- EPE vs EPP foam comparison — The head-to-head between the two polyolefin foams most often confused with each other.